Protecting the conditions around label production
Dry winter air can contribute to static, web clinging, misfeeds and changes in print registration. Paper-based substrates can also curl or change dimensions as they lose moisture.
This 240-by-500-foot facility had a 30-foot ceiling and 3.6 million cubic feet of air. The design target was 40% RH at 70°F. Water quality was part of the plan because mineral residue settling on stock or printing surfaces could affect the process.
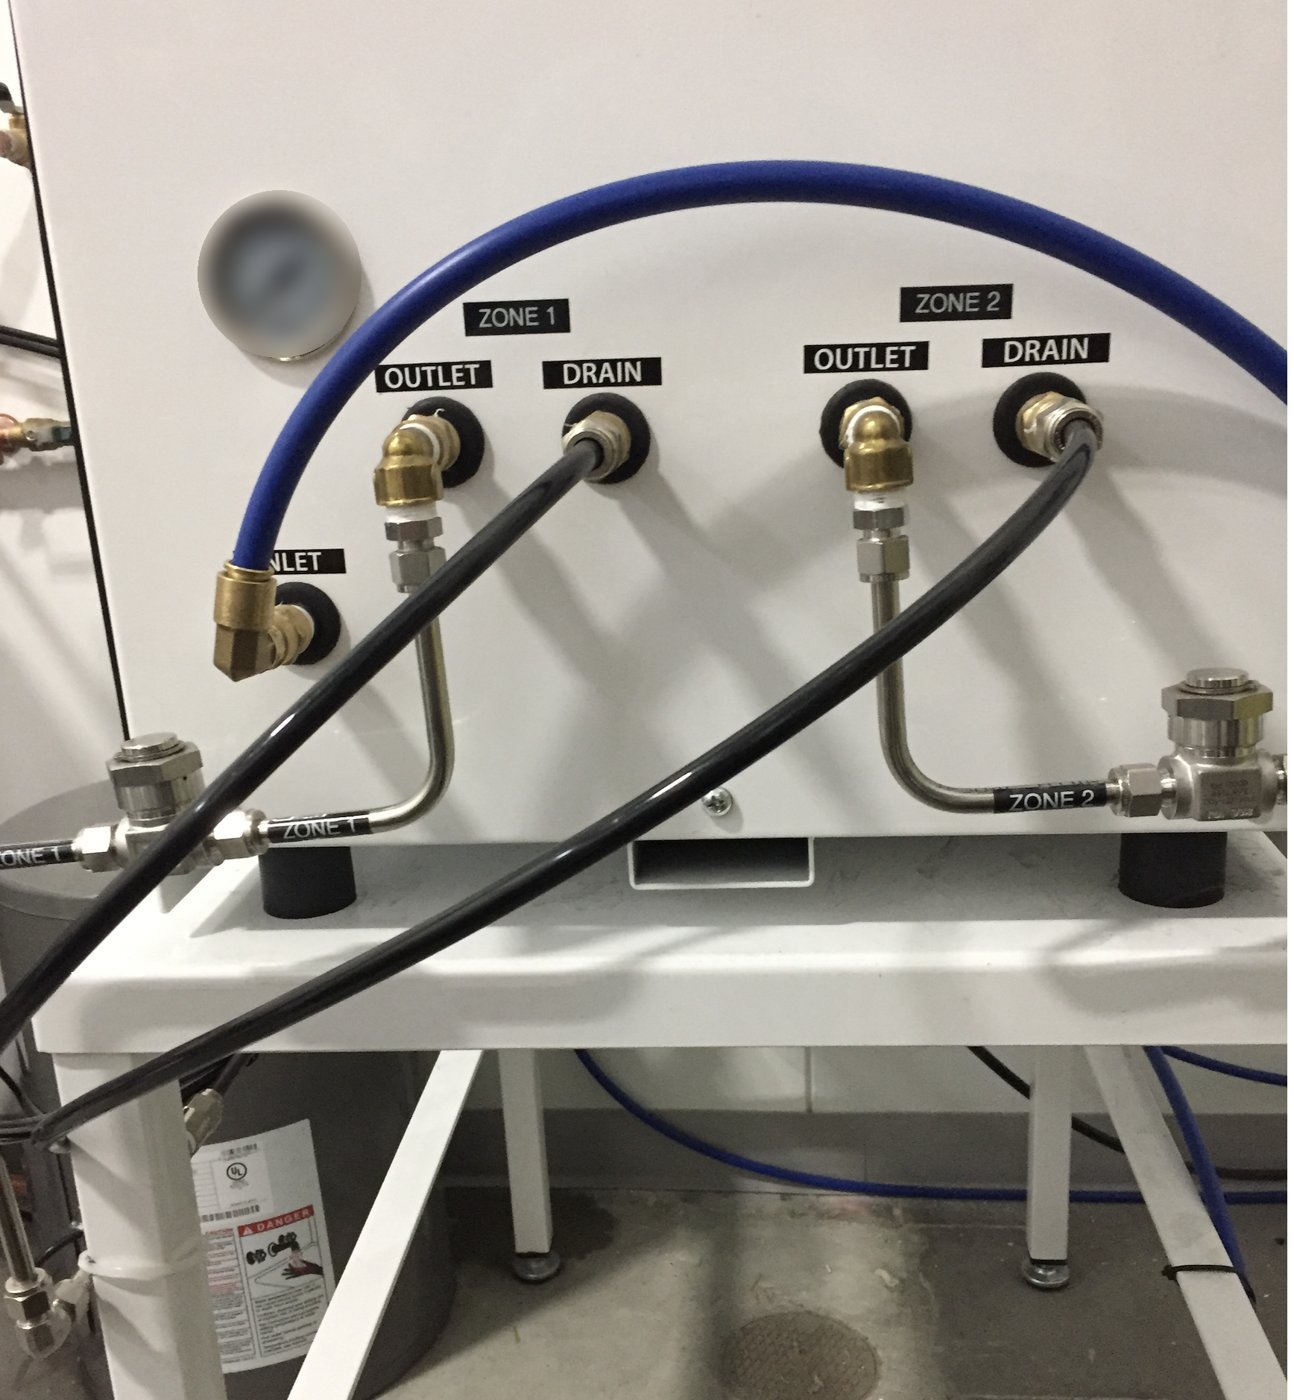
One station serving two zones
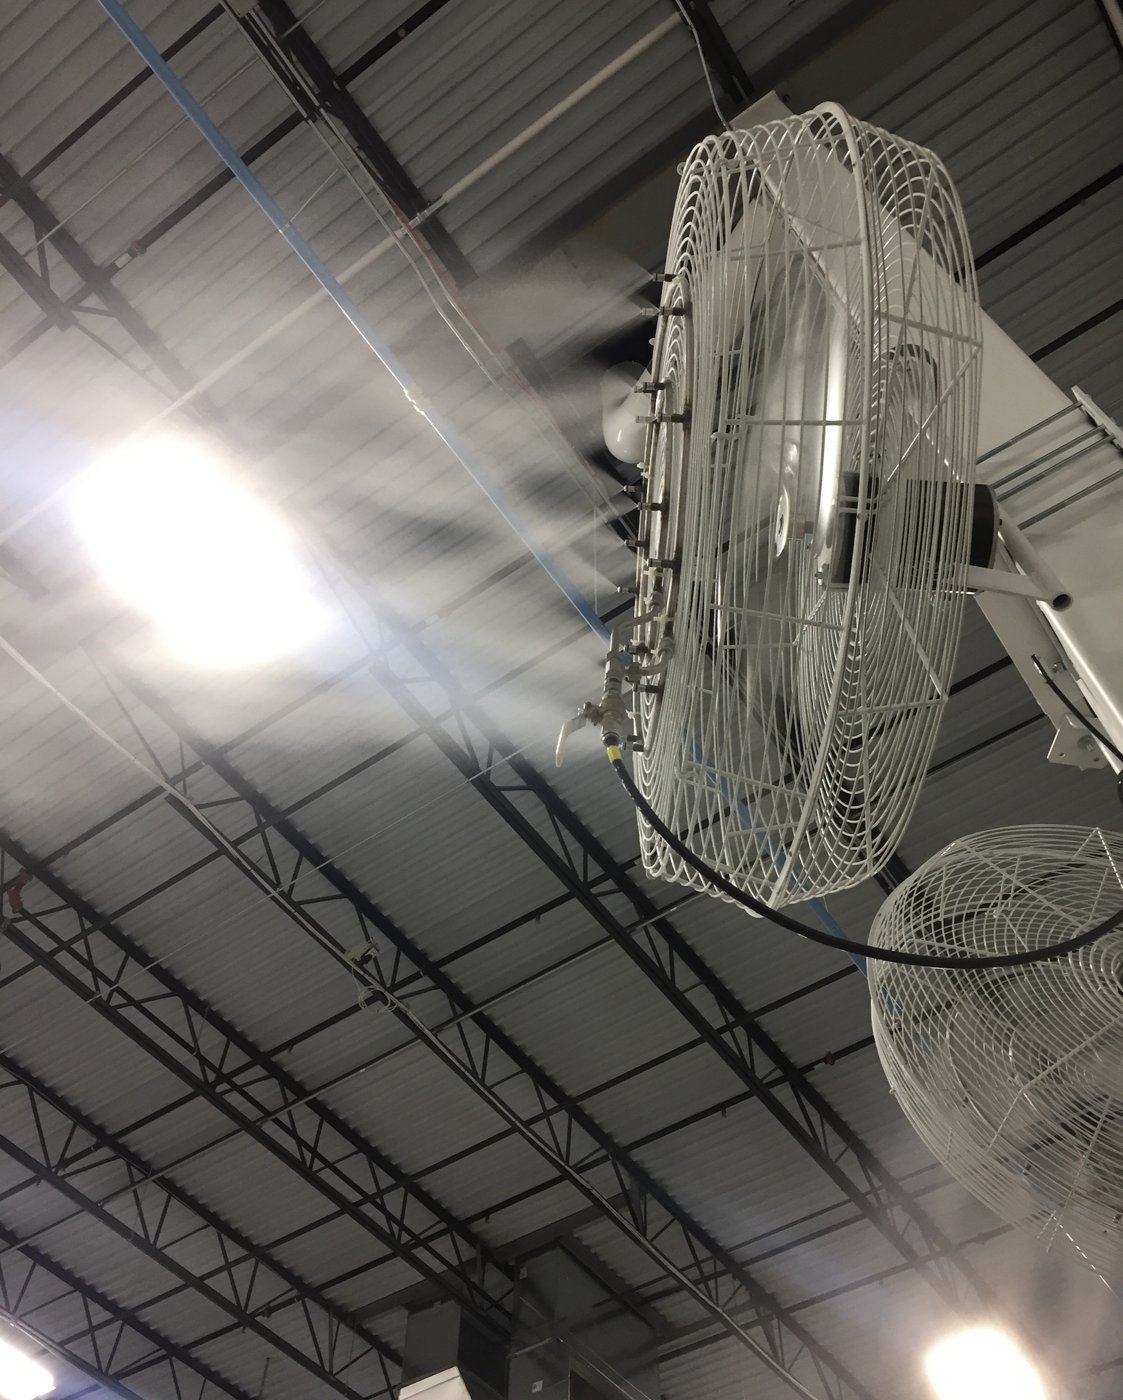
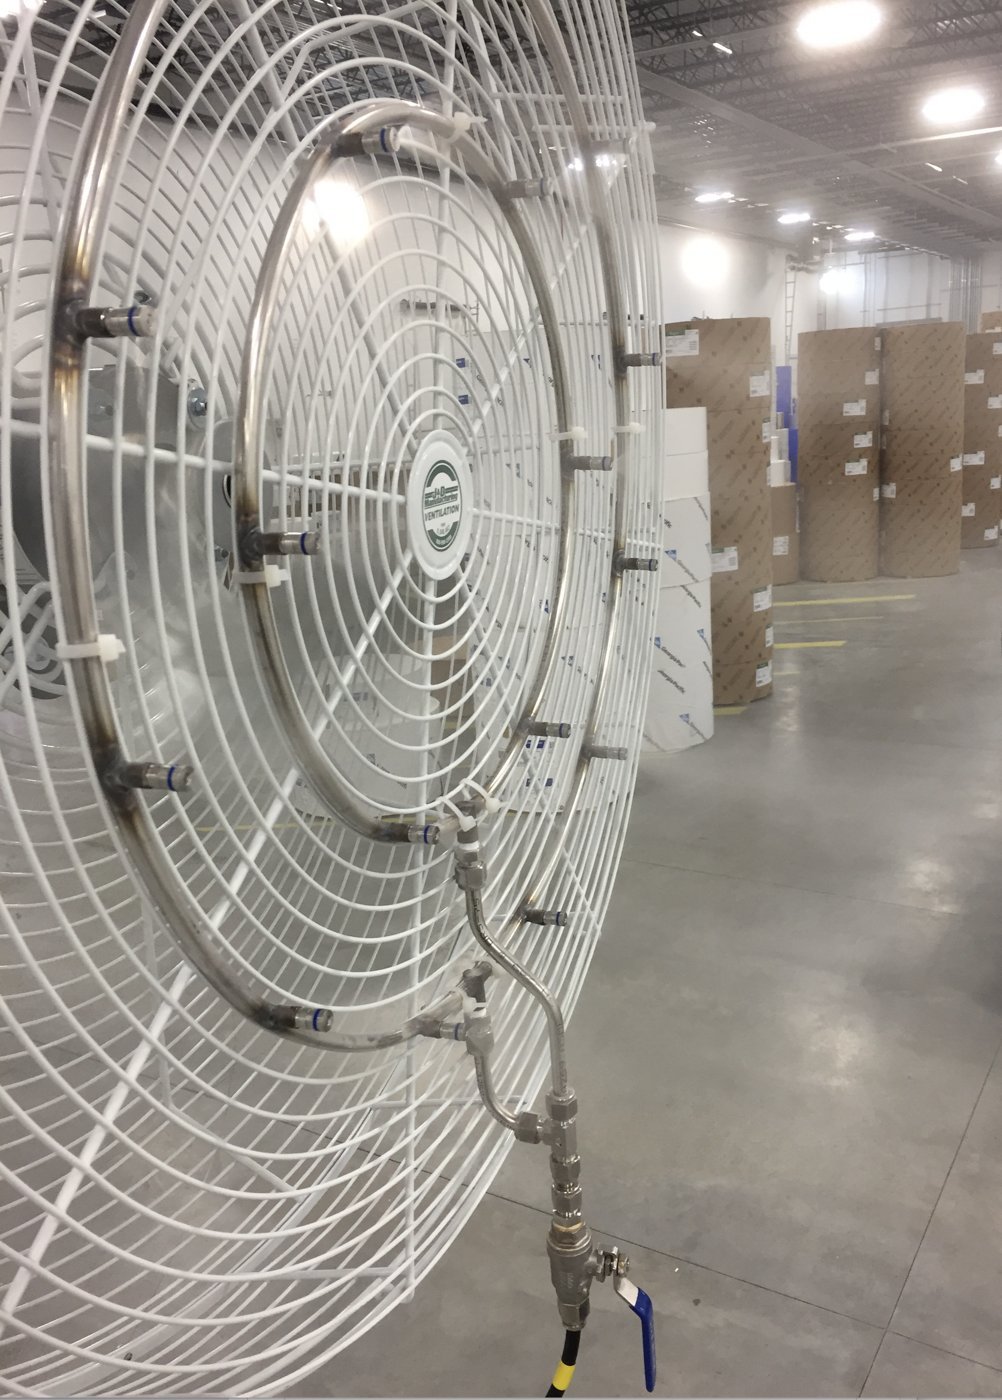
A single 3.8 gpm pump station supplied two independently controlled zones of five fans. Each 36-inch fan used a pair of stainless mist rings: a 24-inch ring with 12 nozzles and a 15-inch ring with six nozzles.
The 180 nozzles were rated at 8 lb/hr each, giving a specified combined output of 1,440 lb/hr. Each zone had its own humidity sensor and controller, working with the pump station's PLC and zone valves.
Deionized water blended to approximately 50 ppm
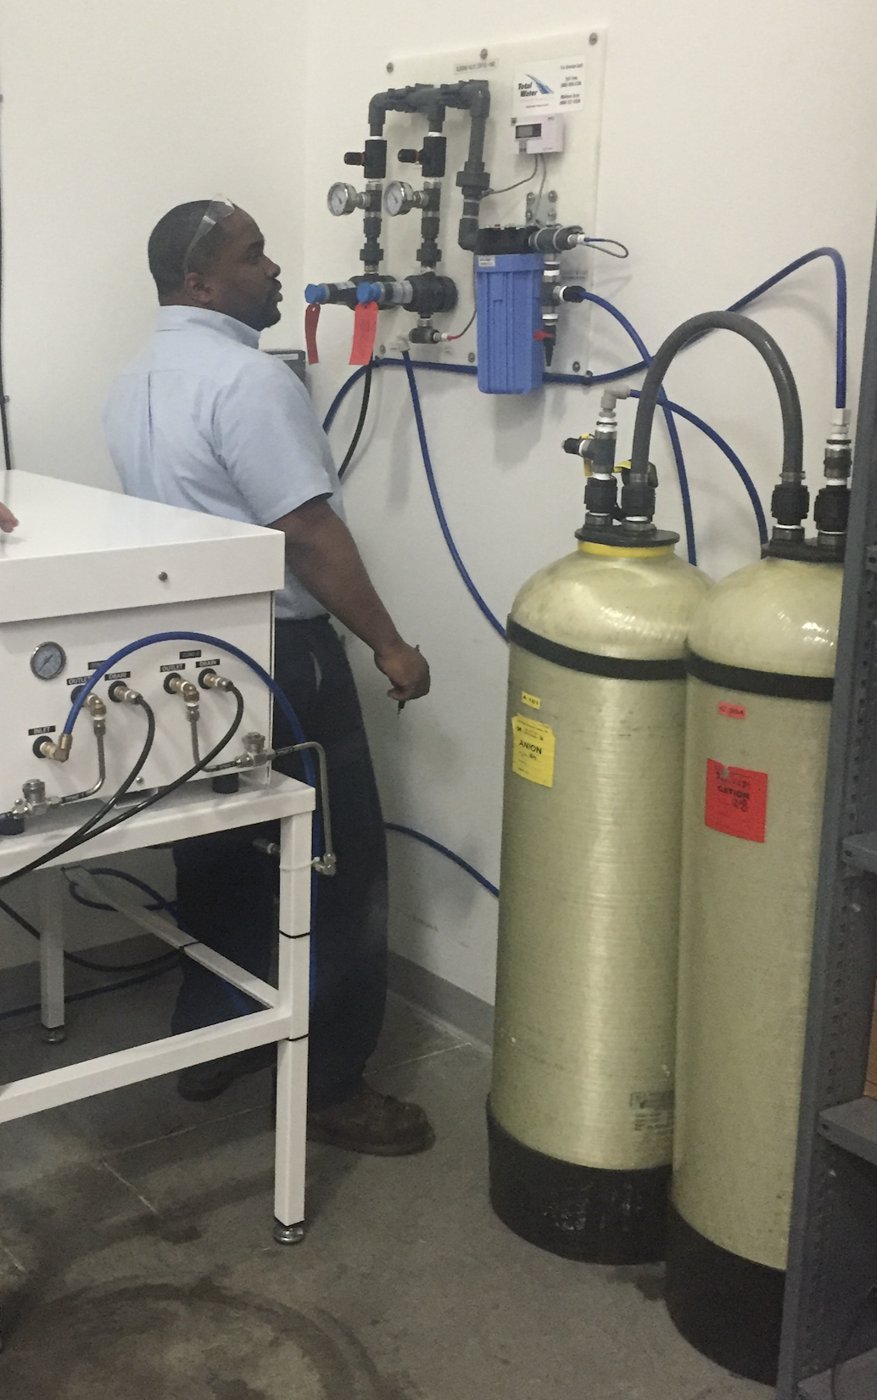
The treatment system used cation and anion deionization tanks to remove dissolved minerals. A blending valve then mixed the treated water with a controlled amount of untreated water to reach approximately 50 ppm total dissolved solids.
The blend was selected to extend the life of the DI resin while maintaining the specified low mineral content. Gauges and a TDS readout allowed maintenance staff to check the supply. This is a project-specific treatment arrangement, not a universal blending specification.
Installation above the production floor
Custom column brackets positioned the fans toward an obstacle-free ceiling space approximately 48 inches across and 20 feet long. Each fan's mist rings were fed through a ball valve.
A two-person installation team completed the work in about two weeks. Rough-in covered the fans, rings, high-pressure tubing and controller wiring. Final work included connections, flushing, startup and operator training. The plant provided supply-water plumbing and electrical service.
Equipment overview
| Equipment | Quantity / configuration |
|---|---|
| 3.8 gpm pump station with two-zone control | 1 |
| Zone humidity controllers and sensors | 2 |
| 36-inch fans with double mist rings | 10 |
| 8 lb/hr anti-drip nozzles | 180 |
| 3/8-inch high-pressure tubing | 1,750 ft |
| Custom column brackets | 10 |
Equipment and ratings describe this project’s original configuration. Contact IHC to confirm current replacement parts and compatibility.
From the installation
Project record
Project completed in November 2016, as recorded in the supplied IHC profile.
Based on the IHC project profile supplied in October 2026. Customer identity and exact location are withheld. RH values are design targets, rather than a continuous operating-performance record.
What does your plant need?
Talk through your building, airflow and production conditions with IHC.
Discuss your facility